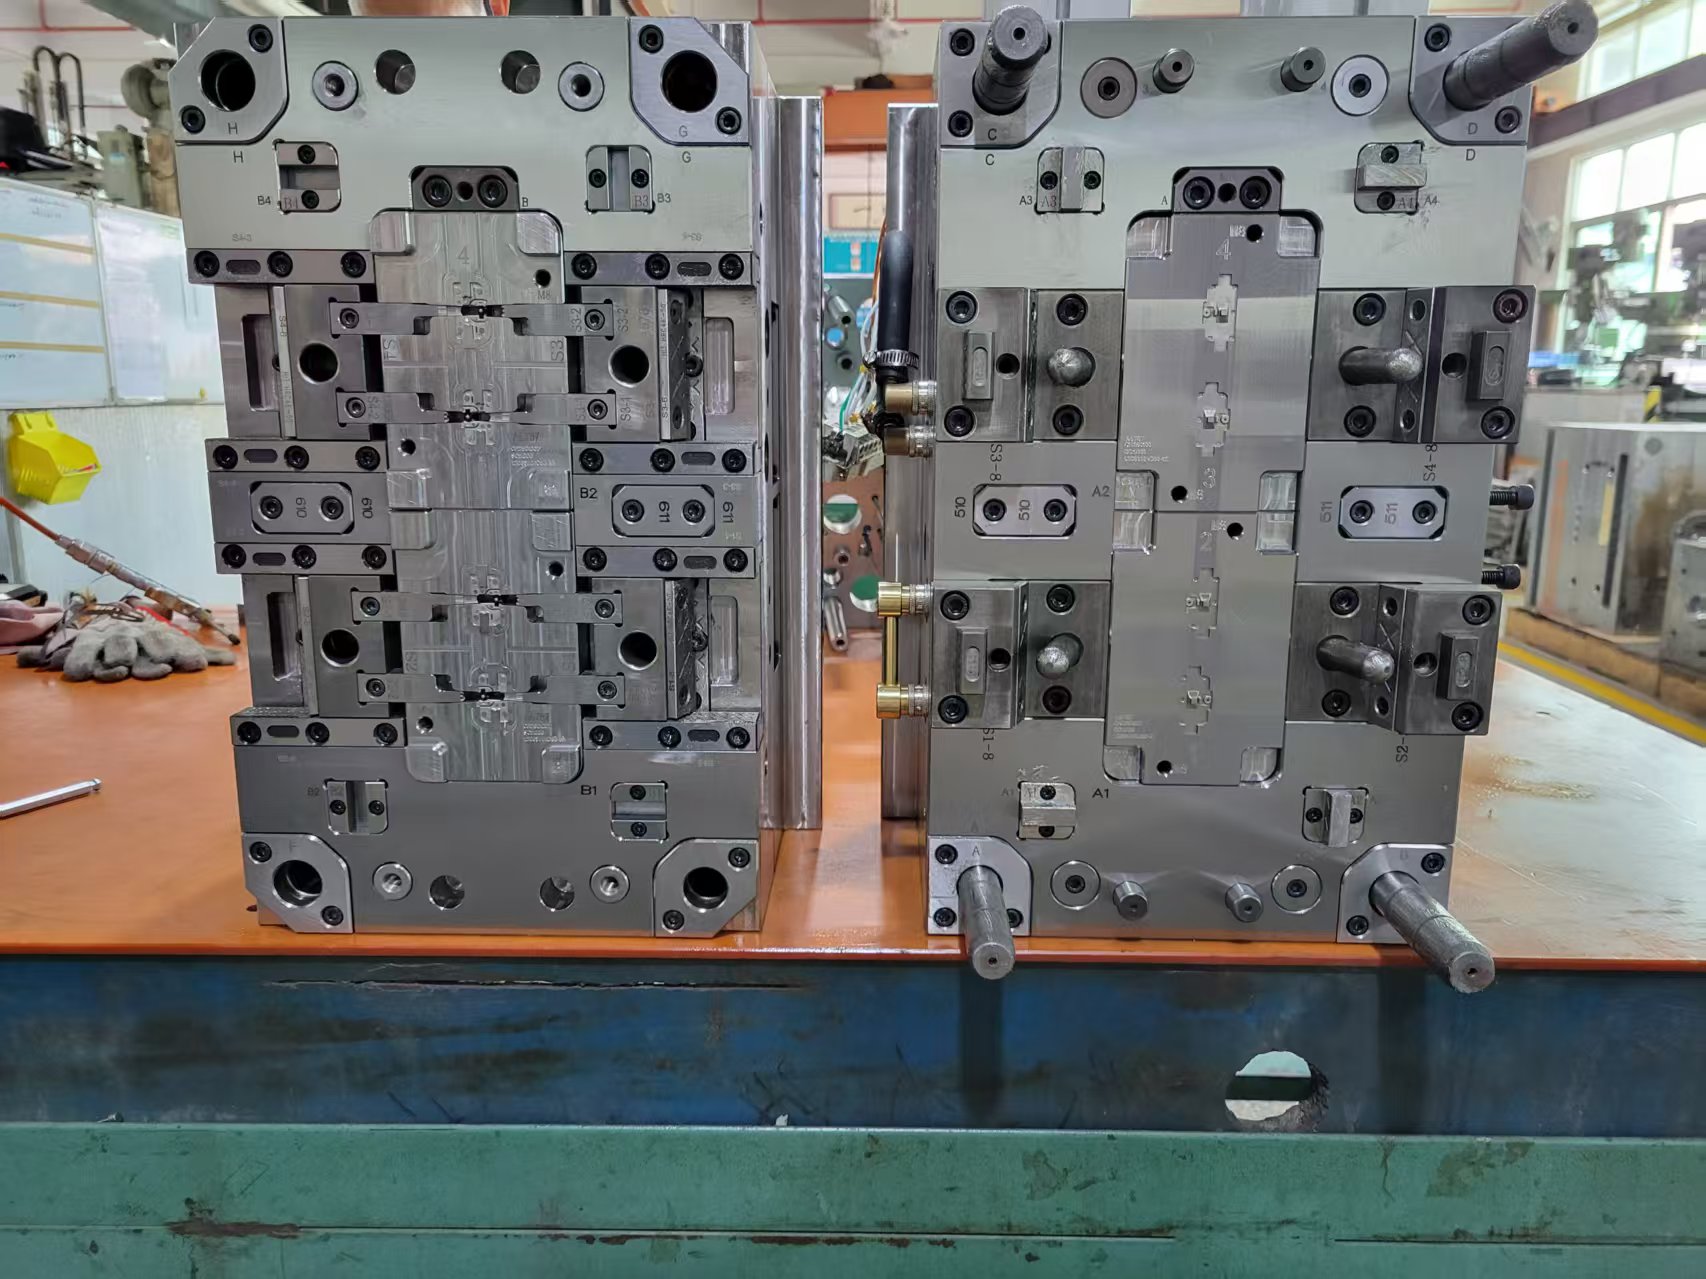
In the manufacturing and mass production of precision injection molds, a tiny deviation at any single stage is transmitted directly to product dimensions, appearance, and even the mold's own service life. For fields with extremely tight tolerance requirements—such as medical consumables and precision electronic components—the mold is not merely a forming tool, but the core asset that determines product yield and compliance. Since its founding in 2005, Jingmu Molds has engraved "precision" into its corporate DNA, controlling machining errors within 0.01 mm through full-process CMM (coordinate measuring machine) measurement, and has built a one-stop precision control system spanning design, manufacturing, and production maintenance. The following systematically breaks down the key control points of precision injection molds across two major phases: during production and after production is completed.
Mold temperature is closely tied to the characteristics of the plastic material and must be controlled strictly and precisely. Frequent mold-temperature fluctuations or scale buildup and blockage in the cooling water circuits cause localized uneven heating of the mold, amplify the stress effects of thermal expansion and contraction, and consequently lead to cavity deformation, steel fatigue, and out-of-tolerance product dimensions.
Pre-production calibration: Before production starts, the temperature controller must be calibrated periodically to ensure the accuracy of its measurement data, providing a reliable temperature reference for subsequent production. For high-temperature specialty materials such as PEEK, a dedicated high-temperature mold temperature controller is required, with barrel temperature reaching 300–400°C.
Operation monitoring: During production, assign dedicated personnel to observe the instrument status in real time, confirming that the cooling lines are unobstructed and the inlet/outlet water temperature differential is under control.
Periodic descaling: Weekly, flush and clean the cooling water circuits to remove scale, sludge, and impurities from the pipe inner walls; monthly, conduct a full inspection of water-line seals and quick couplings to prevent leakage and seepage. Flushing the cooling channels with a high-pressure water gun (0.8 MPa) effectively removes scale and avoids a cooling-efficiency drop of more than 30%.
Depending on part size, part-removal methods mainly fall into three types: fully automatic drop-out, manual removal, and robot (pick-and-place) removal. Regardless of method, the key is to ensure the molded part and the runner system are removed completely and thoroughly.
When the injection machine is in fully automatic mode, "successful part ejection" must be set as the mandatory precondition for entering the next cycle. If a part remains trapped in the mold and clamping continues, it will in most cases damage the mold—and may even cause severe deformation of the precision injection mold.
Jingmu Molds equips the end of the gating system with a highly efficient and reliable sprue puller as standard; the moment the mold opens, it firmly grips and pulls out the cold slug from the sprue and runners, ensuring clean separation of the runner every cycle and structurally eliminating the risk of cold-material residue.
During mass production, the mold operates under harsh conditions of high pressure, high speed, and high temperature; any minor anomaly left unaddressed can escalate into a batch-wide quality incident.
Motion mechanism inspection: Focus on whether the mold's motion sequence is correct, and whether the start/end positions, positioning, and clamping actions of the core-pulling slides are accurate and reliable.
Wear and jamming checks: Closely monitor whether sliding and guide sections show severe wear, and whether ejector pins and return strokes exhibit sticking, breakage, or sluggish movement. Conventional production molds require lubrication replenishment every 8 hours; under high-temperature conditions this must be shortened to 4 hours, and mixing different brands or types of lubricant/grease is prohibited to avoid degradation and caking that cause component jamming.
Digital monitoring: Use a mold monitor to track parameters such as clamping force, ejector-stroke count, and temperature in real time, transitioning scientific injection molding from "experience-driven" to "data-driven."
Every precision mold should be paired with a dedicated history card recording basic information (mold number, steel grade), molding parameters for each use, production shot count, maintenance content, and fault symptoms. This practice makes lubrication, maintenance, and repair fully traceable, and cuts subsequent changeover trial-run time from 2 hours down to 30 minutes. Jingmu Molds documents every trial molding and modification, providing a complete archive for mold life-cycle management.
Impurities generated during injection molding—such as flash and material carbides—if left in the cavities of a precision injection mold, not only affect mold precision and service life but also adversely impact the quality of subsequently produced parts.
Daily cleaning: At the end of each shift, wipe the parting line with a clean cotton cloth, and use a soft copper brush and high-pressure air gun to clear plastic residue, oil stains, and residual plastic on the parting surface from the cavities.
Deep cleaning: After the mold is removed from the injection machine, thoroughly clean the cavities, ejector pins, and cooling circuits; use an ultrasonic cleaner for fine cavity areas and a professional descaler for the cooling water circuits.
No hard tools: Strictly prohibit contact between hard tools such as screwdrivers, hammers, and rigid scrapers and the parting line, cavities, or sealing surfaces, to avoid irreversible scratches.
Certain plastics (such as PVC, POM, etc.) release corrosive gases when thermally degraded, which readily cause rust and corrosion on precision injection molds.
Short-term shutdown (within one week): Immediately after stopping, wipe the mold clean with a soft, lint-free cloth, spray on anti-rust agent, then close the mold; insert uniform anti-rust spacers between the parting surfaces to prevent grease loss.
Long-term idleness (over 15 days): Beyond wiping the cavities, apply grease to key areas and plug the gates; wrap the entire mold in anti-rust film and store it in a dry, ventilated location (temperature 15–25°C, humidity ≤60%), checking the anti-rust condition monthly.
Cooling-circuit protection: Close the inlet/outlet valves and drain residual water from the channels (especially critical in northern winters) to prevent residual moisture from rusting the water lines.
After plastic-part production is complete and before the mold goes into storage, first clean it thoroughly, then conduct a comprehensive inspection of the cavity surface, critical dimension areas, moving components, and locating features to confirm the mold is intact.
Precision re-inspection: Use a 2D measuring instrument (profile projector) or CMM to fully inspect critical dimensions, compare against the original drawing dimensions, and record the deviation trend.
Lubricated storage: Apply sufficient high-temperature grease to all moving parts (ejector pins, slides, guide pillars), and pre-stock identical replacement parts for wear items (ejector pins, seals, springs).
Environmental control: The mold storage environment should avoid humidity, high temperature, and direct sunlight; a constant-temperature, constant-humidity warehouse (temperature 23±2°C, humidity 40–60%) is recommended.
Good maintenance can extend mold life to 2–3 times the original design. Jingmu Molds recommends a four-tier maintenance SOP based on production frequency:
Maintenance tier | Execution cycle | Core content |
Tier 1 | Daily / per shift | Clean cavity residue, spray anti-rust agent, check ejector-pin reset, record mold status |
Tier 2 | Every 50k shots or weekly | Ultrasonic cleaning of cavities, ejector-pin lubrication, cooling-circuit descaling, ejector-pin dimensional sampling |
Tier 3 | Every 200k–500k shots | Full-dimensional precision inspection, wear-part replacement, hot-runner system check, trial-mold verification |
Tier 4 | Annual / over 500k shots | Full mold disassembly, full-dimensional measurement, repair by build-up welding / chrome plating / nitriding, overall heat treatment if necessary |
Competition in precision injection molds ultimately comes down to the depth and consistency of detail control. Jingmu Molds not only controls key-feature tolerances within ±0.005 mm through processes such as slow-wire EDM, precision grinding, and high-speed milling during the machining stage, but also extends these high standards to every clamping and every maintenance act at the customer's site. We firmly believe that only by carrying the philosophy of "prevention first, cleaning priority, regular maintenance" through the mold's entire life cycle can we truly achieve "zero-wait" efficient production and long-term, stable yield output.



 13724506670